A crane rail system must do more than provide a running surface for crane wheels. It must transfer repeated wheel loads into the supporting structure, maintain rail alignment, accommodate operating forces, and remain serviceable under demanding industrial conditions. In facilities where overhead cranes, gantry cranes, or other rail-mounted lifting equipment operate frequently, the performance of the rail support arrangement directly affects equipment reliability, maintenance requirements, and production continuity.
A continuous crane rail support system provides a coordinated method of supporting crane rails along their length. Depending on the engineering design, it may incorporate rail clips, welded rail clips, steel soleplates, elastomeric pads, grout, bolts, and supporting steelwork or concrete foundations. These components work together to secure the rail, distribute loads, control movement, and establish a consistent interface between the rail and its supporting structure.
For industrial project owners, engineering contractors, and procurement teams, choosing the right support arrangement requires more than comparing individual components. The system must match the crane's wheel loads, operating duty, rail profile, support geometry, environmental conditions, and installation requirements.
This guide explains how a continuous crane rail support system works, which components influence its performance, how to evaluate design options, and what to check during installation and long-term maintenance. It also outlines practical considerations for sourcing crane rail fastening components for new construction, equipment upgrades, and rail replacement projects.
1. What Is a Continuous Crane Rail Support System?
A continuous crane rail support system is an arrangement designed to support and restrain a crane rail over a defined length rather than relying solely on isolated contact points. Its configuration depends on the supporting structure, the rail section, the fastening method, and the loads generated by crane operation.
The term continuous describes the intended support arrangement and load-transfer approach. It does not automatically mean that every component extends without interruption along the entire rail length. Some systems use a continuous bearing layer beneath the rail, while others combine a supporting beam or plate with regularly spaced rail fastening assemblies.
The exact arrangement must therefore be established in the project drawings and technical specifications.
1.1 How Continuous Rail Support Works
When a crane wheel passes over a rail, the wheel load travels through several structural interfaces. The rail receives the concentrated load, bends according to its stiffness and support conditions, and transfers the load to the supporting components. These components then transmit the forces to a runway beam, crane girder, concrete foundation, or another engineered support structure.
A typical load path includes:
Crane wheel: Applies vertical loads and may generate horizontal forces during crane travel.
Crane rail: Provides the running surface and distributes wheel loads along the rail.
Rail clips or fastening assemblies: Restrain the rail and help maintain its specified position.
Soleplates or supporting plates: Establish the bearing surface and provide an interface between the rail and the underlying structure where required.
Rubber or elastomeric pads: Provide a defined degree of compliance, cushioning, and contact-pressure distribution when specified.
Grout and anchoring components: Fill designed gaps, establish bearing conditions, or secure the support assembly according to the approved installation method.
Supporting structure: Transfers the combined loads into the building frame, foundation, or other load-bearing construction.
Not every project requires all these components. For example, a crane runway with a machined steel support surface may use a different arrangement from a rail mounted on a concrete foundation with a grouted baseplate.
The engineering objective is to create a predictable load path while keeping the rail within the required alignment and movement limits.
1.2 Continuous Support Versus Discrete Support
A rail can be supported by a continuous bearing arrangement, by discrete support points, or by a combination of these approaches. The distinction matters because the rail's structural behavior depends on how loads are transferred into the supporting structure.
| Consideration | Continuous bearing arrangement | Discrete support arrangement |
|---|
| Bearing contact | Designed to provide bearing along a defined length | Bearing occurs primarily at designated support locations |
| Rail bending | Influenced by rail stiffness and the continuity of the bearing interface | Influenced strongly by rail stiffness and support spacing |
| Load transfer | Can distribute contact pressure over a larger designed area | Transfers loads through individual support locations |
| Installation | Requires control of bearing surface condition and contact | Requires control of support spacing, elevation, and fastening position |
| Maintenance | May require inspection of pads, grout, or bearing interfaces | Often emphasizes clips, fasteners, support points, and local rail condition |
These are general distinctions, not guarantees of performance. A continuous bearing surface does not eliminate rail bending, and a properly engineered discrete support arrangement can perform reliably under its specified operating conditions.
The appropriate design depends on the rail section, wheel-load spectrum, support stiffness, temperature effects, and applicable engineering requirements.
1.3 Where Continuous Crane Rail Support Systems Are Used
Continuous support arrangements may be considered in industrial facilities where cranes operate under repeated or demanding loading conditions.
Common applications include:
Steelmaking and metal processing plants
Foundries and heavy manufacturing workshops
Warehouses with overhead material-handling equipment
Shipyards and fabrication facilities
Power generation and industrial maintenance facilities
Cement plants and bulk-material handling operations
Port terminals and cargo-handling installations
Chemical and process plants
Industrial buildings with long crane runways
Equipment modernization and crane runway rehabilitation projects
The actual support design must reflect the application. A crane handling light materials intermittently may have very different requirements from a process crane operating multiple shifts with frequent loaded movements.
For procurement purposes, identifying the operating environment and crane duty is an important first step toward selecting compatible rail fastening components.
2. Why the Support System Matters to Crane Operation
The rail is only one part of the crane runway. Even a rail manufactured to the correct dimensions can experience premature wear or alignment problems if the underlying support arrangement is unsuitable or incorrectly installed.
A continuous crane rail support system helps engineers manage several interconnected performance requirements.
2.1 Maintaining Rail Alignment
Crane rails must remain within the alignment tolerances established by the applicable project specification. Depending on the installation, these requirements may cover rail gauge, straightness, elevation, horizontal alignment, joint geometry, and relative alignment between parallel rails.
Poor alignment can contribute to uneven wheel loading, increased flange contact, abnormal vibration, and additional forces on crane wheels and runway structures.
Rail clips help restrain the rail in its designed position, but their effectiveness depends on the clip design, fastening method, installation geometry, and the stiffness of the supporting structure. Clips cannot compensate for every underlying structural or alignment problem.
A well-designed support arrangement therefore considers the entire rail installation rather than treating each clip as an independent component.
2.2 Managing Repeated Wheel Loads
Crane rails experience repeated loading as wheels travel along the runway. The magnitude and frequency of these loads depend on crane capacity, wheel arrangement, trolley position, operating cycles, and the distribution of materials being handled.
The support system must be selected for the governing design loads, including relevant dynamic effects and horizontal forces.
Where a continuous bearing layer is used, the bearing surface must be sufficiently uniform to avoid unintended gaps or concentrated contact. Where discrete supports are used, rail stiffness and support spacing must be evaluated together.
Neither approach removes the need for structural calculations. The supporting beam, rail section, fasteners, anchors, and foundation must all be checked against the project's design criteria.
2.3 Controlling Unwanted Rail Movement
During crane operation, the rail may experience lateral forces from wheel guidance, skewing, acceleration, braking, and other operating effects. Depending on the crane configuration, longitudinal forces and thermal movements may also influence the fastening design.
Rail clips and associated fasteners provide restraint within their intended design range. Their function is to maintain the required rail position while accommodating only the movements permitted by the engineering design.
Overly restrictive fastening can create problems if the system must accommodate specified thermal movement. Conversely, insufficient restraint can allow the rail to shift beyond acceptable limits.
The correct balance depends on the rail fastening concept, the location of fixed and movable points where applicable, and the design of the runway as a whole.
2.4 Protecting the Supporting Structure
A rail support system creates an interface between the rail and the underlying steel or concrete. This interface must transfer forces without introducing unacceptable local stresses, bearing gaps, or fastening loads.
Soleplates can provide a suitable mounting surface and help establish the required elevation. Grout can fill designed gaps beneath baseplates or support elements when the installation specification calls for it. Elastomeric pads can modify the contact behavior and provide a degree of compliance where their properties are appropriate.
Each component must serve a defined engineering purpose. Adding a pad, grout layer, or steel plate without checking its effect on stiffness, elevation, and load transfer may introduce rather than solve a problem.
2.5 Reducing Unplanned Maintenance
Maintenance requirements are influenced by the quality of the initial design and installation. Loose fasteners, damaged pads, inadequate bearing contact, rail movement, corrosion, and misalignment can all lead to corrective work.
A coordinated support system makes it easier to define inspection points and replacement procedures. Standardized fastening components may also simplify spare-parts management across multiple runway sections.
However, maintenance savings should not be assumed from the word continuous alone. They depend on actual operating conditions, component durability, installation quality, and the accessibility of the rail for inspection.
3. Main Components of a Continuous Crane Rail Support System
The performance of a continuous crane rail support system depends on compatibility among its components. Buyers should evaluate how the rail, fastening assemblies, bearing surfaces, and supporting structure work together rather than purchasing parts solely by nominal size.
3.1 Crane Rails and Rail Profiles
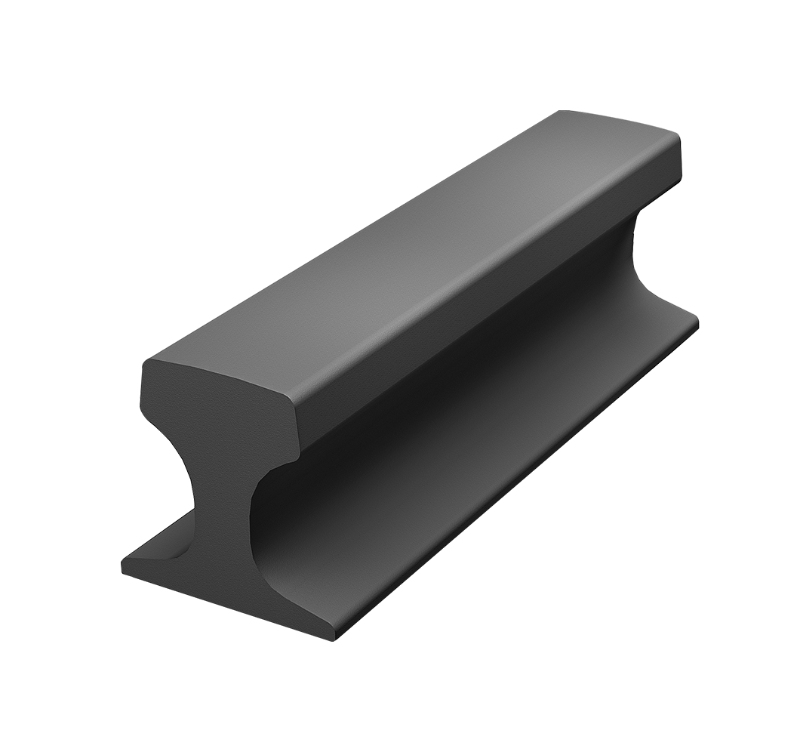
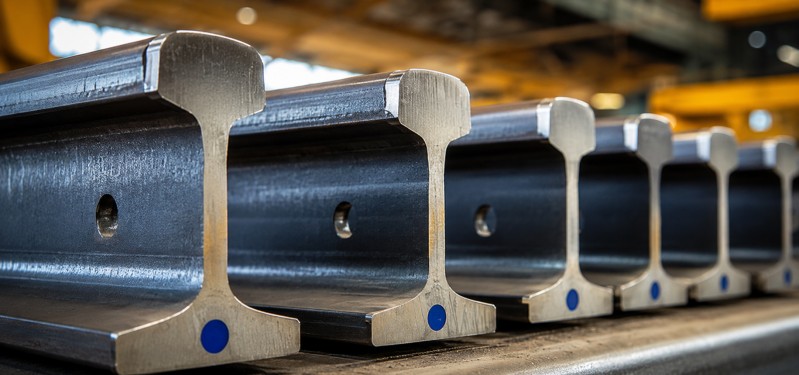
The rail provides the wheel-running surface and distributes wheel loads to the support arrangement. Rail profile, section dimensions, material properties, and straightness influence both structural behavior and fastening compatibility.
Before selecting clips or support plates, confirm the rail designation and dimensional requirements. Two rails with similar overall dimensions may differ in foot width, foot thickness, head geometry, or other features that affect fastening.
The specification should identify the exact rail profile, required material grade, relevant dimensional tolerances, and applicable product standards.
For replacement projects, measure the installed rail and verify its designation rather than relying exclusively on old drawings. Existing rails may have been replaced previously or modified during earlier maintenance work.
3.2 Rail Clips and Welded Rail Clips
Rail clips restrain the rail and help maintain its position relative to the supporting structure. Depending on the design, they may be bolted to a baseplate, attached to a fastening assembly, or welded to a designated steel support component.
Welded rail clips are one option for installations designed around a welded fastening arrangement. Their suitability depends on the rail profile, the geometry of the clip, the welding procedure, the supporting steel, and the forces that must be resisted.
When evaluating welded clips, engineers should confirm:
Compatibility with the specified rail profile
Required lateral and longitudinal restraint
Clip material and mechanical properties
Welding details and permitted welding locations
Accessibility for inspection and maintenance
Corrosion protection requirements
Installation tolerances and replacement procedures
Welding should be performed only at the locations and in the manner approved by the design documentation. Unapproved welding directly to a rail or alteration of a clip can affect material properties, introduce residual stresses, or interfere with the intended fastening behavior.
The appropriate welded rail clip configuration must therefore be selected as part of the complete support design.
3.3 Soleplates and Steel Support Plates
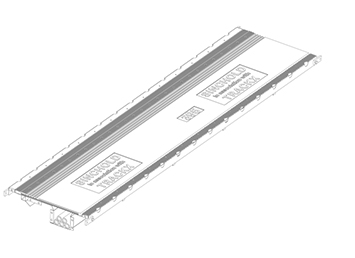
A soleplate provides a mounting or bearing interface between the rail fastening assembly and the supporting structure. It may help establish rail elevation, distribute loads over a defined area, and provide a suitable surface for fastening.
Plate dimensions, thickness, flatness, material, and connection details should be based on the engineering requirements.
A plate that is too flexible may deform under load. A plate with unsuitable dimensions may not provide the required bearing area or fastening edge distances. Poor surface preparation can also affect contact and corrosion protection.
During procurement, specify the plate dimensions and connection details clearly. If machining, drilling, welding, or other fabrication is required, identify these operations in the approved drawings.
3.4 Rubber Pads and Elastomeric Layers
Rubber pads may be incorporated between the rail and its supporting surface to provide cushioning, adjust contact behavior, and help distribute pressure.
Their performance depends on material formulation, thickness, hardness, compression behavior, environmental resistance, and long-term stability under repeated loading.
A pad must be selected for the actual operating conditions. Temperature, oil exposure, water, chemicals, ultraviolet exposure, and contamination may affect material suitability depending on the installation.
Pad thickness also affects the final rail elevation. If the design requires a particular compressed thickness or stiffness, these properties should be defined in the specification.
Elastomeric layers should not be treated as universal solutions for noise, vibration, or alignment problems. Their function must be consistent with the structural design and the characteristics of the rail support arrangement.
3.5 Grout and Bearing Materials
Grout may be used beneath steel plates or other support components to fill designed gaps and establish bearing contact with concrete or another prepared foundation.
The grout specification should consider compressive strength, flow characteristics, placement conditions, curing requirements, environmental exposure, and compatibility with the support geometry.
Before installation, the substrate must be prepared according to the approved procedure. Dust, oil, loose concrete, standing water, and other contaminants can interfere with bonding or bearing quality, depending on the selected material and method.
Grout should not be used to conceal major dimensional errors or replace required structural corrections. Large gaps, inadequate foundation strength, and incorrect support elevations should be addressed through an approved engineering solution.
3.6 Bolts, Anchors, and Fastening Hardware
Bolts and anchors connect rail fastening components to the supporting structure. Their selection affects load transfer, installation accuracy, and the ability to maintain the required fastening condition.
Important parameters include diameter, grade, thread engagement, embedment, corrosion protection, tightening method, and the design loads applied to the connection.
Anchor selection is particularly important when the support arrangement is mounted on concrete. The engineer must verify the anchor type, edge distances, spacing, embedment, concrete condition, and relevant failure modes.
For steel structures, the connection must be checked against the design requirements for the supporting member and the fastening assembly.
Substituting bolts or anchors based only on matching dimensions is not a reliable procurement practice. Mechanical properties and installation requirements must also match the approved specification.
3.7 Supporting Beams and Foundations
The supporting beam or foundation provides the structural base for the rail system. Its stiffness, strength, geometry, and condition influence rail alignment and load distribution.
For a crane runway beam, the engineering assessment may include vertical bending, lateral bending, torsion, local flange behavior, fatigue, deflection, and connection forces as applicable.
For concrete foundations, the assessment may include bearing capacity, cracking, reinforcement details, anchor forces, settlement, and the condition of the mounting surface.
The support system should not be selected independently of these structural checks. A suitable clip and plate assembly cannot compensate for an inadequately designed runway beam or deteriorated foundation.
4. How to Select the Right Continuous Crane Rail Support System
Selection should begin with the operating requirements and supporting structure, not with a catalog item. A technically suitable arrangement must satisfy load requirements, fit the rail profile, accommodate the installation method, and remain accessible for maintenance.
4.1 Confirm the Crane Type and Operating Duty
Start by identifying the equipment and its operating pattern.
Relevant information includes:
Crane type and rated capacity
Number and arrangement of wheels
Maximum wheel loads and load combinations
Frequency of operation
Travel speed and acceleration characteristics
Braking and lateral force requirements
Expected operating cycles
Environmental conditions
Future capacity or operational changes, if planned
Rated lifting capacity alone does not define the rail support requirements. Wheel loads depend on the crane's structural configuration and the position of the lifted load.
Where available, obtain the manufacturer's wheel-load data and the design calculations for the runway. These provide a more useful basis for selecting the support system than an estimate derived from crane capacity alone.
4.2 Identify the Rail Profile and Foot Geometry
Rail fastening components must fit the specified rail. Check the rail designation, foot width, foot thickness, head dimensions, and any other geometry relevant to the clip or support plate.
This is especially important for retrofit projects where the installed rail may differ from the original design.
A clip that fits one profile may not provide the correct contact or restraint on another. Improvised shims or field modifications can change the fastening behavior and should not be introduced without engineering approval.
4.3 Determine the Required Support Arrangement
The design team should establish whether the project calls for continuous bearing, discrete fastening locations, or a hybrid arrangement.
This decision should account for rail stiffness, support spacing, the stiffness of the supporting beam, and the intended load-transfer mechanism.
Where a continuous bearing layer is specified, confirm how bearing contact will be established and inspected. Where discrete supports are specified, confirm the spacing, fastening details, and permissible rail movement.
The specification should describe the intended arrangement clearly enough that the supplier, fabricator, and installer are working to the same design assumptions.
4.4 Evaluate Fastening Restraint and Movement
The fastening system must provide the required restraint without interfering with intended movement.
The engineer should determine the lateral restraint requirements, longitudinal restraint conditions, and whether thermal expansion must be accommodated at designated locations.
Rail clips should be selected according to the approved load requirements and rail geometry. For welded arrangements, the design must also define the welding details, materials, and quality-control procedures.
Do not assume that a more rigid fastening system is automatically preferable. The correct configuration is the one that satisfies the specified structural and movement requirements.
4.5 Check Environmental Conditions
The operating environment affects material selection and expected service life.
For indoor installations, relevant factors may include temperature variation, dust, lubricants, and industrial chemicals. Outdoor installations may also face rain, standing water, ultraviolet exposure, temperature cycling, and atmospheric corrosion.
Marine facilities, chemical plants, and other aggressive environments may require specific coating systems, corrosion-resistant materials, or additional inspection measures.
The specification should identify the environmental conditions and required corrosion protection for each relevant component. A coating suitable for one environment may not be adequate for another.
4.6 Consider Installation and Replacement Access
A support arrangement may be technically suitable but difficult to install or maintain in a restricted location.
Check whether installers can access fastening points, apply the required tightening procedure, perform welding safely where applicable, and inspect completed connections.
For operating facilities, replacement work may need to be completed during short shutdown windows. In these situations, component standardization, accurate drawings, clear installation procedures, and spare-parts availability can help reduce disruption.
The total installation method should be reviewed before the component order is finalized.
4.7 Compare Total Project Requirements
The purchase price of individual clips or plates does not represent the complete cost of a rail support system.
A more useful evaluation considers material supply, fabrication, installation labor, welding or grouting work, alignment adjustments, inspection, access equipment, maintenance, and replacement requirements.
For projects with long runways, even small differences in installation time per fastening location can affect the overall schedule.
Procurement teams should therefore compare complete technical offers on a consistent scope. Confirm which components, fabrication operations, technical documents, and quality records are included in each quotation.
5. Installation Procedures and Quality Control
Installation quality is a major factor in the performance of a continuous crane rail support system. The work must establish the specified rail geometry, provide the intended bearing conditions, and ensure that fastening components are installed according to the approved design.
The following workflow provides a practical framework. Actual procedures must follow the project drawings, engineering specifications, and applicable safety requirements.
5.1 Review Drawings and Inspect Delivered Components
Before installation begins, review the latest approved drawings and confirm that the delivered materials match the bill of materials.
Check the rail profile, clip designation, plate dimensions, bolt specifications, pad thickness, grout requirements, and other relevant details.
Inspect components for visible damage, deformation, corrosion, missing parts, and incorrect machining. For critical components, verify the required material certificates and inspection records.
Any discrepancy should be resolved before installation. Field adjustments made without documented approval can create alignment and load-transfer problems that are difficult to identify after the rail is in service.
5.2 Survey the Supporting Structure
The supporting beam or foundation must be checked before the rail is installed.
Survey the support elevation, straightness, horizontal alignment, connection condition, and other dimensions required by the project specification.
For concrete installations, confirm that the foundation has reached the required condition for the planned work. Verify anchor positions and the condition of the mounting surface.
For steel runways, inspect the support geometry and confirm that the relevant connection details are complete.
If the measured structure falls outside the permitted tolerances, obtain an approved corrective procedure before proceeding. Rail clips should not be used to compensate for major errors in the supporting structure.
5.3 Establish the Required Rail Position
Set out the rail line using the survey control points and installation tolerances specified in the drawings.
Check rail gauge where parallel rails are installed, along with elevation, straightness, joint position, and the relationship between the rail and the supporting structure.
Temporary positioning equipment may be used to hold the rail during adjustment, provided it does not interfere with the approved installation procedure.
The goal is to establish the correct rail geometry before final fastening. If the rail is secured while misaligned, later corrections may require loosening fasteners, adjusting the support arrangement, or removing installed components.
5.4 Install Soleplates, Pads, or Bearing Materials
Where soleplates are specified, install them according to the approved dimensions and fastening details. Confirm their orientation, elevation, and contact with the supporting surface.
Where elastomeric pads are used, check their type, dimensions, placement, and condition. Pads should be free from contamination and positioned as specified.
Where grout is required, follow the product-specific mixing, placement, and curing instructions. Confirm that the prepared surface and installation conditions meet the approved method.
Do not proceed to the next stage until the bearing arrangement has been checked. Unintended gaps, displaced pads, or improperly seated plates may affect the final rail elevation and load distribution.
5.5 Position and Secure the Rail Clips
Install rail clips in the locations and orientations shown in the approved drawings.
For bolted systems, verify the specified bolt type, washers, thread engagement, and tightening method. Apply the required torque or other defined tightening procedure where applicable.
For welded rail clips, confirm the approved welding procedure, welder qualifications, base material requirements, and permitted welding locations. Inspect completed welds according to the specified acceptance criteria.
The rail must remain within the required alignment tolerances during fastening. Tightening or welding should not pull the rail into an unintended position.
The installation team should also confirm that clips provide the intended restraint and that no component has been modified without approval.
5.6 Check Rail Joints and Welded Connections
Rail joints are important locations for inspection because geometric discontinuities can affect wheel passage and local loading.
Check joint position, end alignment, gaps where specified, and the condition of any joint bars or associated components.
Where rail welding is part of the project, the welding procedure must be appropriate for the rail material and the intended service conditions. Required inspection and testing should be completed before the rail is accepted for operation.
Rail welding and clip welding are different operations with different purposes. The procedures, personnel qualifications, and inspection criteria should be specified accordingly.
5.7 Perform Final Alignment and Fastening Checks
After the rail is installed, carry out the final survey and compare the measured results with the project tolerances.
The inspection should cover the applicable parameters, including:
Rail straightness and horizontal alignment
Rail elevation and level
Gauge between parallel rails
Rail joint geometry
Fastener position and installation condition
Required bolt tightening records
Weld quality and inspection records
Bearing surface condition
Pad and grout condition where applicable
Completion of specified corrosion protection
Record the results in the project quality documentation. If a measurement is outside the permitted range, correct the issue through the approved process and repeat the relevant inspection.
5.8 Complete Commissioning Checks
Before the crane returns to normal operation, verify that the installation has met the specified acceptance requirements.
The commissioning procedure may include visual inspection, dimensional verification, confirmation of fastening records, and controlled operational checks as required by the project.
Any test movement should follow the crane manufacturer's instructions and the site's commissioning plan. Personnel should remain clear of hazardous areas, and any abnormal noise, vibration, movement, or wheel interaction should be investigated.
A completed installation record helps establish a baseline for future maintenance and provides evidence that the support system was inspected before service.
6. Common Installation Problems and How to Prevent Them
Many crane rail problems develop from a combination of design, fabrication, and installation issues. Identifying these risks early can reduce corrective work and improve the consistency of the finished runway.
6.1 Uneven Bearing Contact
Uneven contact beneath the rail or support plate can create localized loading and affect the intended load path.
Potential causes include an irregular supporting surface, incorrect plate geometry, improperly positioned pads, or inadequate grout placement.
Prevention begins with a survey of the supporting structure and inspection of the bearing interface before the rail is finally secured.
If a gap or bearing defect is identified, determine its cause and follow the approved correction method. Do not simply add material or tighten fasteners in an attempt to force the components into position.
6.2 Incorrect Clip Selection
A clip with unsuitable geometry may not fit the rail profile or provide the required restraint.
This can occur when procurement uses an approximate rail designation, when an existing rail has been replaced with a different profile, or when a nominally similar component is substituted without engineering review.
To prevent this problem, include the exact rail designation, clip type, dimensional requirements, and applicable drawings in the purchase documentation.
Where necessary, require dimensional verification or sample approval before releasing the full production order.
6.3 Inconsistent Fastener Installation
Inconsistent bolt tightening can affect the fastening condition. Under-tightening may fail to achieve the intended connection performance, while excessive tightening can damage components or introduce unwanted stresses.
The correct method depends on the fastener design and the connection specification. A generic torque value should not be applied to every rail fastening assembly.
Use the specified tightening procedure, suitable tools, and documented inspection requirements. If the design calls for a particular tightening sequence, follow that sequence consistently.
6.4 Poor Welding Quality
Welded fastening arrangements depend on the quality of the weld and the suitability of the welding procedure.
Potential defects may arise from unsuitable preparation, incorrect welding parameters, contamination, inadequate welder qualification, or welding in an unapproved location.
The project specification should define the required welding procedure and inspection method. Visual inspection alone may not be sufficient where additional testing is required.
Welding records should identify the relevant procedure and inspection results so that the completed work can be traced during acceptance and future maintenance.
6.5 Incorrect Rail Elevation
Rail elevation errors may result from incorrect support dimensions, unsuitable plate thickness, misplaced pads, or insufficient control during grout installation.
These errors can affect the relationship between the rail and the crane wheels, as well as the alignment between parallel runways.
Establish the required elevation from reliable survey control points. Check the support arrangement before final fastening and repeat the survey after installation.
Any adjustment must preserve the intended bearing and fastening conditions.
6.6 Inadequate Corrosion Protection
Corrosion can affect rail clips, bolts, plates, welds, and supporting steelwork. Its severity depends on the environment, protective coating, material selection, and maintenance practices.
Pay particular attention to locations where water or industrial contaminants can accumulate, and to surfaces damaged during handling or installation.
The specified protection system should be compatible with the operating environment and the component's intended service conditions. Repair damaged coatings according to the approved procedure.
6.7 Incomplete Installation Records
Missing records make it harder to confirm that the rail support system was installed correctly and to identify changes during later maintenance.
Typical documentation includes material certificates, dimensional inspection results, welding records, bolt tightening records where required, grout documentation, alignment surveys, and nonconformance reports.
Define the documentation requirements before installation begins. This allows contractors and suppliers to prepare the necessary records as work progresses instead of attempting to reconstruct them at project completion.
7. Continuous Crane Rail Support System Maintenance
Maintenance should be based on the crane's operating conditions, the support system design, manufacturer recommendations, and the applicable inspection requirements.
A practical maintenance program combines routine visual checks with scheduled dimensional inspections and more detailed examinations when evidence of abnormal behavior is found.
7.1 Inspect Rail Clips and Fasteners
Look for loose or displaced components, damaged clips, missing fasteners, corrosion, and visible deformation.
For bolted assemblies, follow the specified inspection and tightening procedure. Do not automatically retighten every fastener without considering the connection design, because the correct inspection method depends on the assembly and its intended preload or restraint condition.
For welded assemblies, check for visible cracking, corrosion, deformation, or other signs of damage. Any suspected weld defect should be assessed according to the applicable inspection procedure.
Where repeated defects occur at the same location, investigate the underlying cause rather than replacing the component without further analysis.
7.2 Monitor Rail Alignment and Wear
Changes in rail alignment may develop gradually due to support movement, structural deformation, fastening problems, or operational forces.
Scheduled surveys can help establish whether the rail remains within the required tolerances. The appropriate inspection frequency depends on operating duty, observed conditions, and the maintenance plan.
Inspect the rail running surface for abnormal wear, damage, and local defects. Uneven wear patterns may indicate a problem with wheel interaction, alignment, or load distribution.
Measurements should be compared with established baseline data and the acceptance criteria applicable to the installation.
7.3 Examine Pads and Bearing Interfaces
Where pads are installed, inspect for visible displacement, deterioration, extrusion, or other changes that may affect the intended bearing behavior.
For grouted support arrangements, look for cracking, separation, crumbling, or evidence that the bearing interface has changed.
Not every visible crack indicates structural failure, and not every defect can be assessed reliably from appearance alone. Significant changes should be reviewed against the original design and evaluated by qualified personnel.
Repairs should restore the intended bearing and load-transfer conditions rather than simply cover the visible defect.
7.4 Investigate Abnormal Noise and Vibration
New or increasing noise and vibration may indicate rail joint problems, wheel defects, alignment changes, loose components, or changes in the support interface.
These symptoms are not specific to one failure mode. A structured investigation should consider the crane wheels, rail geometry, fastening system, supporting structure, and operating conditions.
If a defect presents an immediate safety risk or the equipment exceeds its permitted operating condition, follow the site's equipment shutdown and inspection procedures.
Maintenance teams should record the location, operating circumstances, observations, and corrective actions so that recurring issues can be identified.
7.5 Maintain a Consistent Inspection Record
A useful maintenance record includes the inspection date, rail section, fastening locations checked, measured deviations, observed defects, repair actions, and the responsible personnel.
Photographs and measurement data can help compare conditions over time. Recording recurring problems by location may also reveal patterns related to crane travel, wheel loading, environmental exposure, or support geometry.
These records help maintenance planners determine which areas need closer attention and whether the original support design remains suitable for the current operating duty.
8. Continuous Crane Rail Support Systems for Different Industrial Environments
Although the basic engineering principles remain similar, operating conditions can change the priorities for rail support selection.
8.1 Steel Plants and Foundries
Steel plants and foundries may expose crane runway components to high ambient temperatures, dust, scale, impact, and demanding operating cycles.
Material selection, thermal conditions, corrosion protection, and inspection access require careful consideration.
The support arrangement must be designed for the actual temperature range and load spectrum. Components should not be selected solely on the basis of nominal load capacity if the environment introduces additional material or maintenance requirements.
Where production interruptions are costly, spare-part standardization and accessible inspection points can help maintenance teams plan repairs efficiently.
8.2 Warehouses and Manufacturing Workshops
Warehouses and manufacturing facilities often use overhead cranes for repetitive material handling. Depending on the crane duty, consistent alignment and reliable fastening may be important for limiting unnecessary wheel and rail wear.
Support selection should consider the building structure, rail spacing, crane travel frequency, and the possibility of future equipment changes.
If a facility plans to increase lifting capacity or operating frequency, the existing runway should be assessed before the crane or support components are upgraded.
A replacement clip with the correct physical dimensions does not automatically make an existing runway suitable for a higher design load.
8.3 Ports and Outdoor Crane Installations
Outdoor crane systems may be exposed to moisture, temperature changes, wind-related operating conditions, and corrosive atmospheres.
Corrosion protection should be specified for the rail fastening components, supporting steelwork, and associated hardware. Drainage and access for inspection also deserve attention.
For outdoor systems, thermal movement and the overall structural arrangement may be particularly important. The design must account for the expected temperature range and the movement permitted by the rail fastening concept.
Maintenance procedures should include inspection of exposed connections and areas where water or debris can accumulate.
8.4 Chemical and Process Facilities
Chemical and process facilities may expose support components to aggressive substances, cleaning agents, oils, or other contaminants.
Material and coating selection should be based on the actual exposure conditions. General descriptions such as chemical resistant are not sufficient for selecting a component for a specific process environment.
Where the chemical identity and concentration are known, provide this information to the supplier or materials engineer so that compatibility can be assessed.
The installation design should also consider whether maintenance access is restricted and whether replacement work requires special shutdown or safety procedures.
8.5 Existing Crane Runway Rehabilitation
Rehabilitation projects require additional attention because the original support structure and installation records may be incomplete.
Before selecting replacement components, assess the condition of the rail, supporting beam or foundation, fastening points, and any existing plates or pads.
Check whether the installed rail profile matches the available drawings. Confirm the actual wheel loads and operating duty, particularly if the crane has been upgraded or the production process has changed.
A replacement support system should be compatible with the existing structure and the intended future operating conditions. Where the existing structure is damaged or outside the required tolerances, structural correction may be necessary before new fastening components are installed.
9. How to Specify and Purchase Crane Rail Support Components
For B2B buyers, a clear technical specification reduces ambiguity between the engineering team, component manufacturer, fabricator, and installation contractor.
The purchase package should provide enough information for the supplier to confirm compatibility and identify any missing engineering inputs.
9.1 Prepare a Technical Inquiry Package
A useful inquiry package typically includes the following information.
Project information
Project name and installation location
New construction, replacement, or rehabilitation
Indoor or outdoor operating environment
Planned installation and commissioning schedule
Crane and load information
Crane type and rated capacity
Maximum wheel loads and wheel arrangement
Operating duty and travel conditions
Required lateral and longitudinal restraint
Applicable structural design criteria
Rail information
Rail designation and profile dimensions
Rail material and required standard
Rail length and joint arrangement
Required alignment tolerances
Existing rail condition for replacement projects
Support and fastening information
Supporting beam or foundation details
Required support arrangement
Clip type and installation method
Soleplate dimensions and material
Pad or grout requirements, where applicable
Bolt, anchor, and welding specifications
Corrosion protection requirements
Quality and documentation requirements
Required material certificates
Dimensional inspection requirements
Welding procedure and inspection records
Applicable testing and acceptance criteria
Packaging, marking, and traceability requirements
Providing this information helps the supplier evaluate the intended application and reduces the need for repeated clarification during quotation and production.
9.2 Confirm the Scope of Supply
The term rail fastening system can refer to different combinations of components. One supplier may quote clips only, while another may include plates, bolts, pads, and related accessories.
Compare quotations on the basis of a clearly defined scope.
Confirm the quantity and type of each component, whether fabrication is included, what installation accessories are supplied, and which technical documents will accompany the shipment.
For projects requiring installation support, clarify whether the scope includes rail installation, welding, grouting, alignment, inspection, or commissioning assistance.
These services should be stated explicitly rather than assumed to be included in a component quotation.
9.3 Verify Compatibility Before Mass Production
For a project involving many fastening locations, confirming component compatibility before mass production can reduce rework.
The review may include dimensional drawings, interface details, sample inspection, or an engineering review of the proposed assembly.
Pay particular attention to rail foot geometry, clip contact surfaces, bolt positions, plate dimensions, and the relationship between the fastening system and the supporting structure.
If a substitute component is proposed, require documented confirmation that it meets the relevant design and specification requirements.
A visually similar product should not be accepted as equivalent without technical verification.
9.4 Evaluate Manufacturing and Quality Control
Rail fastening components operate in a structural application and should be purchased against defined material and quality requirements.
When assessing a manufacturer, review the production capabilities relevant to the ordered components. These may include machining, forming, casting or forging where applicable, welding, surface treatment, assembly, dimensional inspection, and material traceability.
The required manufacturing processes depend on the component design. Not every supplier needs every process, but the supplier must be able to control the processes used for the specific order.
Buyers should also establish how nonconforming components are identified, documented, and corrected. Clear inspection criteria are more useful than general statements about quality.
9.5 Consider Delivery and Project Coordination
Crane rail projects often involve multiple interfaces among civil engineering, structural steel fabrication, rail supply, crane installation, and electrical or mechanical commissioning.
Late delivery of a small fastening component can delay a larger installation sequence if the component is required before the rail can be secured.
Confirm the production schedule, inspection milestones, packaging method, shipment quantities, and delivery documentation.
For projects with phased installation, coordinate component deliveries with the construction sequence and available storage conditions.
Where several rail profiles or clip types are used, clear labeling and traceability can reduce the risk of incorrect components reaching the installation area.
9.6 Evaluate Technical Support
Supplier support is useful when a project involves unusual rail profiles, difficult installation conditions, nonstandard support geometry, or rehabilitation of an existing runway.
A capable technical team should be able to review the supplied drawings, clarify component dimensions, explain installation requirements, and identify information needed for a compatibility assessment.
The supplier's role must remain clear. Structural calculations and final system approval should be completed by the responsible engineering parties unless the supplier has explicitly been contracted and qualified to provide those services.
This division of responsibility helps ensure that product selection, structural design, and installation are coordinated without leaving critical requirements undefined.
10. Working with a Crane Rail Fastening System Manufacturer
A manufacturer specializing in rail fastening components can support procurement by supplying products to defined technical requirements and coordinating component details with the project team.
For buyers sourcing rail clips, welded rail clips, plates, bolts, and related fastening components, the objective is to obtain a consistent product package that matches the approved design and can be installed and inspected efficiently.
Sinchold is an integrated manufacturer and solution provider in the rail systems industry, with capabilities covering research and development, design, manufacturing, and support for rail fastening systems. Its product scope includes rail clamps, soleplates, rubber pads, grouts, and related components, alongside rail installation services.
The company operates a production facility in Nantong and established Sinchold KSA (SFCC) in Dammam in 2024 to strengthen its presence in the Middle East. This local presence is relevant to project teams seeking regional coordination and support for rail-related infrastructure work.
When evaluating Sinchold or any other potential supplier, buyers should define the required rail profile, load conditions, fastening arrangement, installation method, and quality documentation. These details provide the basis for determining whether the proposed components are suitable for a particular application.
10.1 Welded Rail Clips for Project-Specific Applications
Welded rail clips may be considered where the approved design uses a welded connection between the clip and a designated support component.
Their selection should take account of rail geometry, required restraint, supporting steel details, weld design, and maintenance access.
For a project that specifies welded clips, the inquiry should identify the intended rail profile and provide the relevant drawings. The engineering team should also define the welding procedure and acceptance criteria.
The final selection should be based on technical compatibility and the approved project design rather than on the product category alone.
10.2 Coordinating Related Rail System Components
A crane rail support arrangement may require more than one fastening component. Depending on the design, the supply package may include clips, plates, rubber pads, bolts, anchors, grout, or other related items.
Coordinating these interfaces during procurement can help avoid dimensional conflicts and incomplete deliveries.
For example, plate thickness and pad thickness influence the installed rail elevation. Bolt dimensions must match the fastening geometry, and the selected clip must fit the rail profile. Grout requirements must be consistent with the designed bearing interface.
These details should be reviewed together before production and installation.
10.3 Planning for International Industrial Projects
International projects may involve multiple engineering organizations, different documentation requirements, long shipping distances, and local installation contractors.
A clear technical inquiry helps suppliers understand the required scope and prepare consistent documentation. Buyers should specify the governing standards, units, inspection requirements, packaging, delivery location, and expected schedule.
For projects in the Middle East, coordination among the project owner, engineering consultant, contractor, and supplier is particularly important when installation activities must align with a defined construction sequence.
Local support can assist with communication and project coordination, but the technical acceptance criteria must still be defined by the project requirements.
11. Frequently Asked Questions About Continuous Crane Rail Support Systems
What is a continuous crane rail support system used for?
A continuous crane rail support system provides a coordinated arrangement for supporting and restraining crane rails along a runway. Depending on the design, it may help establish bearing contact, distribute loads, maintain rail position, and transfer forces into the supporting structure.
Its suitability depends on the rail profile, crane loads, support geometry, fastening method, and operating environment.
Does continuous support mean the rail has no gaps beneath it?
Not necessarily. The term describes the intended support concept, but the actual bearing arrangement depends on the system design.
Some systems use a continuous bearing layer, while others use regularly spaced fastening assemblies or a combination of continuous and discrete support elements. The drawings and technical specifications should define the required bearing condition.
What is the difference between a rail clip and a welded rail clip?
A rail clip is a component used to restrain a rail in its designed position. A welded rail clip is intended for a fastening arrangement that uses a specified welded connection to a designated support component.
The installation method, connection details, and maintenance requirements differ. The correct type depends on the approved rail fastening design.
Can welded rail clips be used with every crane rail?
No. Compatibility depends on the rail profile, clip geometry, material, support arrangement, welding details, and required restraint.
The rail and clip should be checked against the project drawings before procurement. Unapproved modifications or welding at unspecified locations should be avoided.
Are rubber pads necessary beneath crane rails?
Rubber pads are not required in every installation. They are used when the design calls for a particular bearing interface, degree of compliance, or other defined function.
Their material, thickness, and mechanical properties must suit the operating conditions. A pad should not be added or removed without confirming the effect on the system design.
What information is required to select crane rail fastening components?
The main inputs include the rail designation and dimensions, maximum wheel loads, crane operating duty, support structure details, required restraint, environmental conditions, and applicable standards.
For welded clips, the approved welding details and supporting steel geometry are also important. For concrete-mounted systems, anchor and foundation information must be provided.
How often should a crane rail support system be inspected?
There is no single inspection interval suitable for every crane runway. The frequency should follow the applicable regulations, equipment manufacturer's recommendations, project requirements, operating duty, and observed condition.
Facilities with demanding duty cycles or aggressive environments may need more frequent inspections. Inspection results should be recorded and used to adjust the maintenance plan where appropriate.
What causes crane rail fastening problems?
Common causes include incorrect component selection, rail misalignment, unsuitable bearing conditions, inconsistent fastening installation, welding defects, corrosion, structural movement, and inadequate maintenance.
Repeated problems should be investigated to identify the underlying cause rather than addressed only through component replacement.
Can an existing crane runway be upgraded with a new support system?
An upgrade may be possible, but the existing rail, supporting structure, fastening points, and operating loads must be assessed first.
The proposed components must fit the actual rail geometry and meet the intended load and restraint requirements. If the crane capacity or operating duty is changing, the runway structure may also require reassessment.
What should buyers compare when sourcing rail support components?
Buyers should compare technical compatibility, material requirements, manufacturing quality, dimensional accuracy, inspection documentation, installation requirements, delivery scope, and technical support.
Price should be evaluated against an equivalent technical scope. A quotation that excludes necessary accessories, fabrication, or documentation may not represent the same project cost as a complete supply package.
12. Conclusion: Selecting a Support System Around Real Operating Requirements
A continuous crane rail support system is an engineered interface between the crane rail and the supporting structure. Its performance depends on the interaction of rail geometry, fastening components, bearing conditions, structural stiffness, installation accuracy, and maintenance practices.
For engineering and procurement teams, the most important step is to establish the operating requirements before selecting individual components. Confirm the maximum wheel loads, rail profile, support arrangement, required restraint, environmental conditions, and applicable acceptance criteria. Then evaluate clips, soleplates, pads, bolts, anchors, grout, and supporting structures as parts of the same load-transfer system.
Installation quality is equally important. Accurate surveying, suitable bearing preparation, correct fastening procedures, controlled welding, and documented final inspections help establish a reliable baseline for operation. Routine maintenance can then identify changes in alignment, fastening condition, corrosion, and bearing performance before they develop into more serious problems.
For new construction and rehabilitation projects, clear technical specifications also improve communication among suppliers, contractors, and engineering teams. They reduce uncertainty during quotation, help prevent incompatible substitutions, and make quality verification more straightforward.
Sinchold provides rail fastening products and related rail system support, including welded rail clips, rail clamps, soleplates, rubber pads, grouts, and rail installation services. Buyers planning a crane rail project can review the welded rail clips product range and prepare a technical inquiry based on their rail profile, support configuration, operating loads, and installation requirements.
A well-specified support arrangement is not defined by one component alone. It is defined by how the complete system performs under the loads, movements, and environmental conditions it is designed to handle.
 CN
 EN
 RU
 DE
 FR
 ES
 PT
 AR


 Sinchold
 Oct 27 2026
 Sinchold


 Recommended news